 English
 ไทย
 日本語
 한국어
Screw counting versus torque and angle records: what each can prove
A count, a tightening measurement and a traceability record are different evidence. Specify the acceptance question first: number of operations, measured torque/angle, or a record linked to the workpiece. Then confirm the equipment and process that can support it.
| Capability | What to specify | Limit to confirm |
|---|---|---|
| Screw counting | Configured operation count, reset and station signals | Does not alone prove actual joint torque, angle or every screw position |
| Torque / angle measurement | Measured tightening values with a confirmed transducer/tool/controller setup | Does not alone establish workpiece ID linkage, storage or MES integration |
| Traceability | Required record fields, workpiece ID, storage, export and retrieval process | Must confirm firmware, interface and integration scope; not implied by a counter |
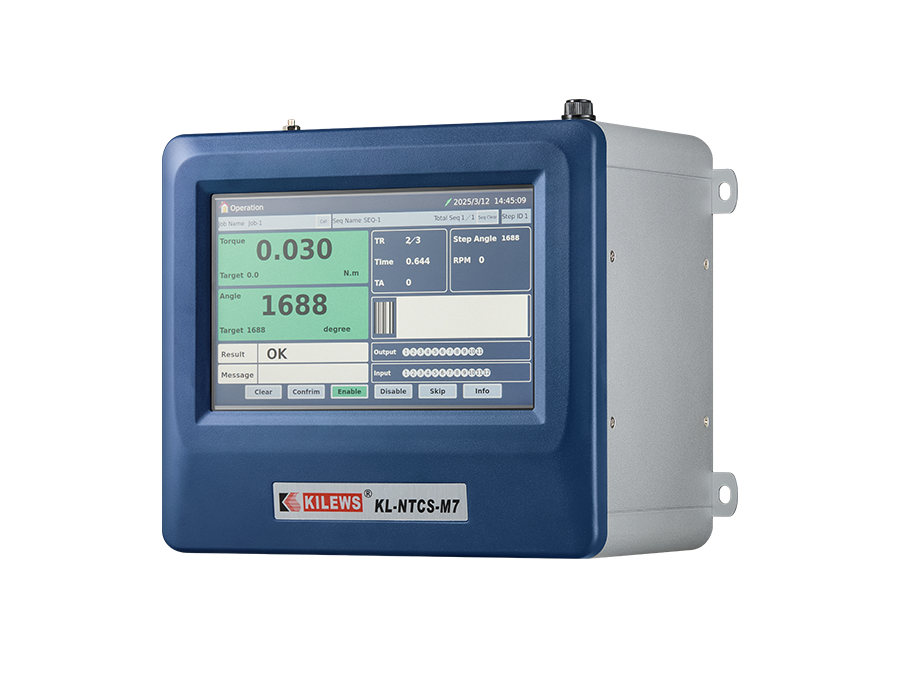
The reviewed BE200L/BE500L examples list an integrated LED screw counter. SNT-CSM103/106/110 and KL-NTCS-M7 belong to the transducer tightening system; confirm tool/controller/cable, process settings and the records required for the job. A published interface or record capacity does not guarantee connection to every PLC/MES.
Keep units separate when reviewing the SNT-CSM103/106/110 model table: 0.375–3, 0.75–6 and 1.25–10 are kgf.cm; the N.m cells are “-”. A tool specification or controller accuracy statement is not itself proof of the final joint result.
Questions before specifying the order
Can a correct count still leave an assembly problem?
Yes. Count logic does not by itself establish the correct screw position, measured torque, joint condition or part quality. Validate missed/double operations, reset, rework and any required interlocks on the real station.
Does a transducer system automatically include a traceability project?
No. Specify workpiece ID, required torque/angle/status fields, retention, export, access and PLC/MES protocol. Confirm hardware, firmware, cable and software/integration scope in writing.
How should a counting trial be defined?
State screws per workpiece, operator sequence, count/reset criteria, abnormal and rework cases, required signals and acceptance evidence. Confirm the detection behaviour of the exact device.
What should be sent for quotation?
Provide the current tool/controller, target torque/unit, number of screws, process sequence, abnormal cases, required measurements/records, interface details, quantity and receiving date.
Reviewed product and purchasing sources
Brushless model comparison · Assembly station checklist · Quotation, stock and delivery · Contact KILEWS Thailand
For a multi-item quotation, add products from their model pages to the existing inquiry list. State exact models, configuration and quantities; ask sales how to send drawings or labels. Reading this guide does not place an order.
Get selection support
Our Thailand team helps with tool selection and system matching.